Thermal & Chemical Resilience
Polyurethane (PU) flooring systems are hybrid cementitious resin systems. Unlike standard epoxy, polyurethane coatings are specifically formulated to exhibit high thermal elasticity. This means they expand and contract at the same rate as the concrete beneath them during thermal shocks (such as boiling water washdowns or high-pressure steam cleans in dairy or beverage units), preventing delamination.
Our PU screeds are seamless, slip-resistant, and inherently antimicrobial. They contain active silver-ion based additives that inhibit bacterial growth on the floor's surface, making them a necessity for USDA and food processing compliance.
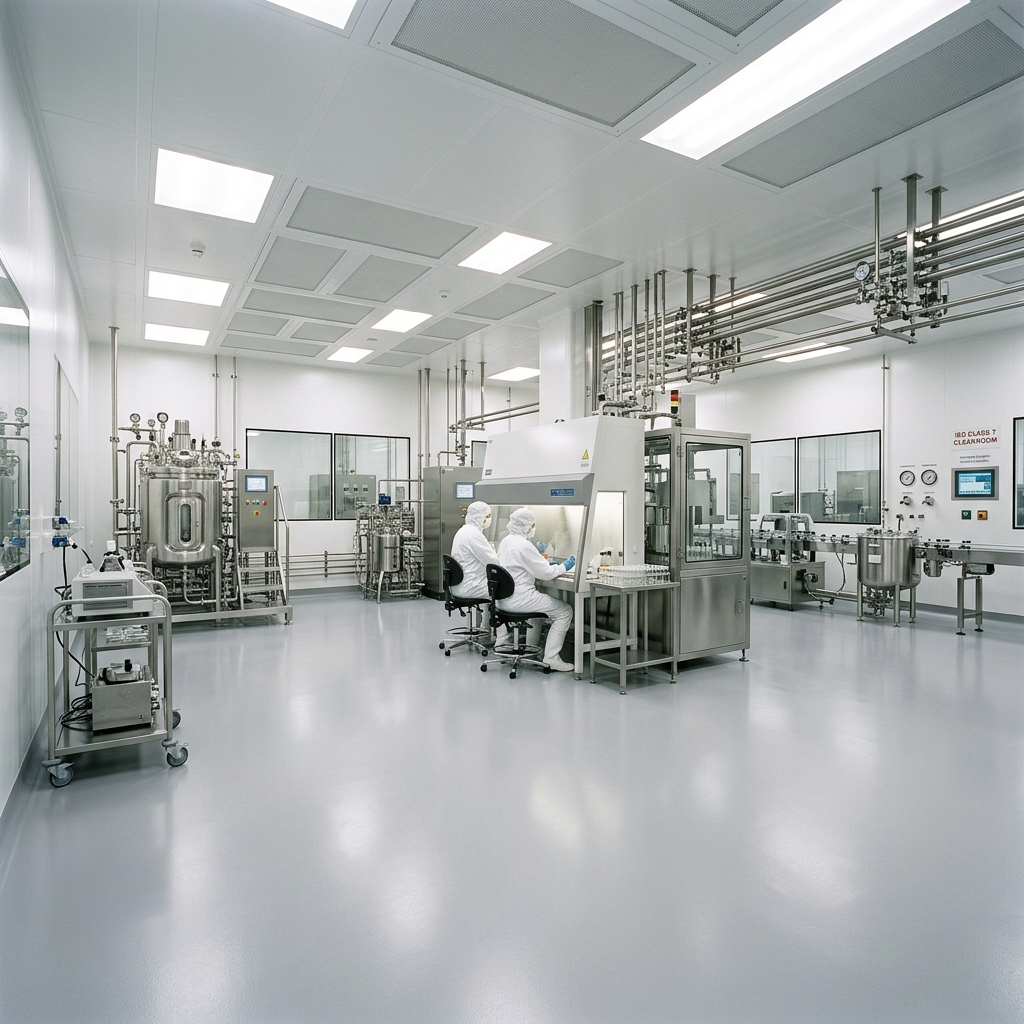
Our Specialized PU Products
- HI-TECH EP PRIMER (Epoxy Primer) Is a complete solid epoxy resin adhesion promoter. It is Eco-friendly, low in VOC count, solvent-free with a high level of mechanical and chemical resistance.
- HI-TECH EPC PRIMER (Epoxy Primer) Is a two-component epoxy primer designed to penetrate concrete pores, consolidate the substrate, and provide a strong bonding surface for subsequent epoxy and PU coatings.
- HI-TECH WB PRIMER (Epoxy Water Based Primer) Is a two-part, solvent-free, water-based resin primer with low viscosity, is commonly applied as an under-layer primer on highly porous substrates before the resinous primer application.
-
HI-TECH
FLOORGIENE MD (Polyurethane Self-Levelling Topcoat)
Is a four-component coloured polyurethane floor finish with antimicrobial properties, applied smoothly in a matte texture at a thickness of 3-6 mm.
Key Advantages: Antimicrobial, Chemical Resistant, Hygienic, Temperature Resistant, Abrasion Resistant
Application Area: Pharmaceutical Plants, Chemical Plants, Food & Beverages Plants, Warehouse & Storage Area, Poultry/Meat/Fish Plants, Hotel & Kitchen, Dairy & Milk Product
Standard Colours: Blue, Yellow, Green, Grey, Light Grey, Red
-
HI-TECH
FLOORGIENE SL (Polyurethane Self-Levelling Topcoat)
Is a four-component polyurethane flooring system designed for high-performance industrial floor applications. Protects floors subject to heavy traffic, abrasion, and chemical exposure with a smooth matt coloured finish, generally applied at a thickness of 2mm.
Key Advantages: Antimicrobial, High Chemical Resistance, High Thermal Resistance
Application Area: Pharmaceutical Plants, Chemical Plants, Food & Beverages Plants, Warehouse & Storage Area, Poultry/Meat/Fish Plants, Hotel & Kitchen, Dairy & Milk Product
Standard Colours: Blue, Yellow, Green, Grey, Light Grey, Red